Vacuum formed fenders are used across signage and wayfinding because they can be produced without the tooling spend of injection moulding and without the weight of sheet metal. This page covers how 10 mm HIPS sheet is formed for signage and wayfinding, what tolerances are realistic, and what has to be on the drawing before tooling starts.
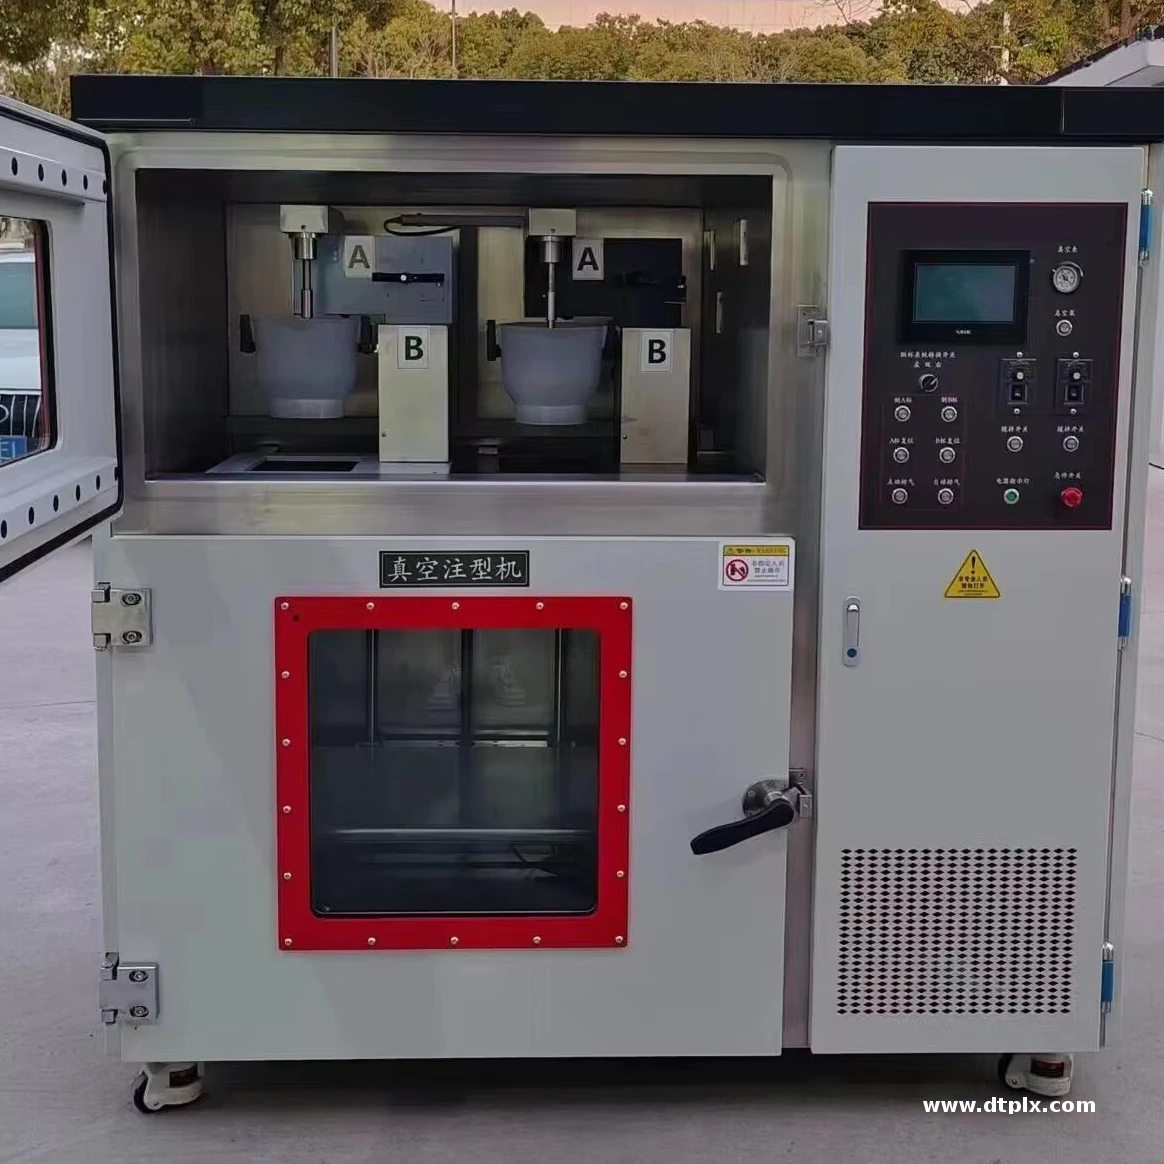
The route below is the one used for most of the fenders shipped from this plant: sheet is heated on the forming machine, drawn over an aluminium or composite mould, cooled on a jig, then trimmed on a 5-axis router. For fenders the sheet gauge is selected from the load case rather than from habit, and HIPS is the material most often specified for this combination.
| Item | Value |
|---|---|
| Part type | fenders |
| Industry | signage and wayfinding |
| Material | HIPS |
| Sheet thickness | 10 mm (1.5–12 mm available) |
| Maximum forming area | 3,000 × 2,000 mm |
| Typical tolerance | ±0.5 mm formed, ±0.2 mm on trimmed edges |
| Tooling | aluminium for production, composite for samples |
| First article | 7–15 working days |
| Production lead time | 3–4 weeks after approval |
| Finish | as formed, textured, painted or printed |
HIPS is the low cost route for indoor liners and disposable trays where impact strength is not critical.
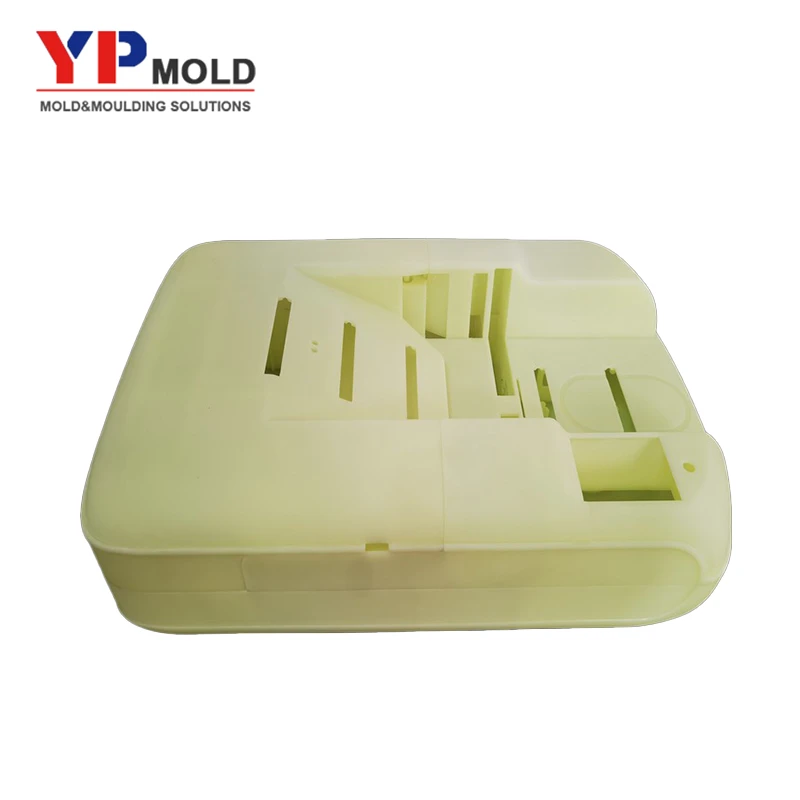
First article inspection covers critical dimensions, wall thickness, colour and texture against the approved sample. Sheet thickness is checked on the formed part at the points shown on the drawing, and the readings go into the report.
Tooling is the main cost driver at low volume, so a 10 mm fenders for signage and wayfinding is usually quoted with a composite or printed mould first and the aluminium tool cut once the design is frozen. That keeps the first article cost low and gives a real part to test before the production tool exists. The result is shorter lead time compared with the alternatives, and a piece price that stays stable across repeat releases.
Yes. Send a sample or scan and the part can be reverse engineered, with the wall thickness and material measured from the sample.
Sample and first article tooling is usually cut in 7 to 15 working days. Production aluminium tools take 3 to 4 weeks depending on size and cooling layout.
A 3D file or drawing, the material if it is fixed, the annual quantity and the finish. Photos of the current part are enough for a first estimate.
Send the drawing or a photo of the current fenders with the quantity and the finish. The first reply is a manufacturability review with the wall thickness, material and a quotation, so the decision is made on facts rather than on a price alone.
Send the 3D file or drawing with your quantity — manufacturability review and quotation within 24 hours.
Leave a Message