A rail transit interiors manufacturer came to us with equipment covers produced as a machined aluminium housing. The parts worked, but the cost and the lead time were holding up the programme. This is how they were reworked as vacuum formed equipment covers in 12 mm TPO, and what the change delivered over the first 400 pieces.
The previous machined aluminium housing needed several operations to reach finished shape, and every operation added both cost and a chance for variation. Weight was higher than it needed to be, and design changes meant new fixtures each time. For a programme of 400 pieces a year that is a poor fit.
| Item | Value |
|---|---|
| Process | thick gauge vacuum forming, 5-axis CNC trimming |
| Material | TPO at 12 mm |
| Forming area used | up to 3,000 × 2,000 mm |
| Tooling | aluminium production mould with a composite sample tool first |
| Finish | as formed gloss |
| Batch size | 50 pieces per release |
| First article | 6 weeks from drawing release |
| Documentation | dimensional report, material certificate, first article inspection |
“The sample arrived on the date we were given and it fitted the assembly on the first try. The equipment covers is lighter than the part it replaced and the finish holds up in the field. We now release the equipment covers against stored tooling and the paperwork comes with the shipment.”
If the part is a shell, cover, tray or enclosure between 1.5 mm and 12 mm thick, it is almost always worth quoting. Send the drawing and the answer comes back with a material and a tooling plan.
Tooling, trim fixtures and programmes are kept against the part number for the life of the programme, so a repeat release needs no new proving run.
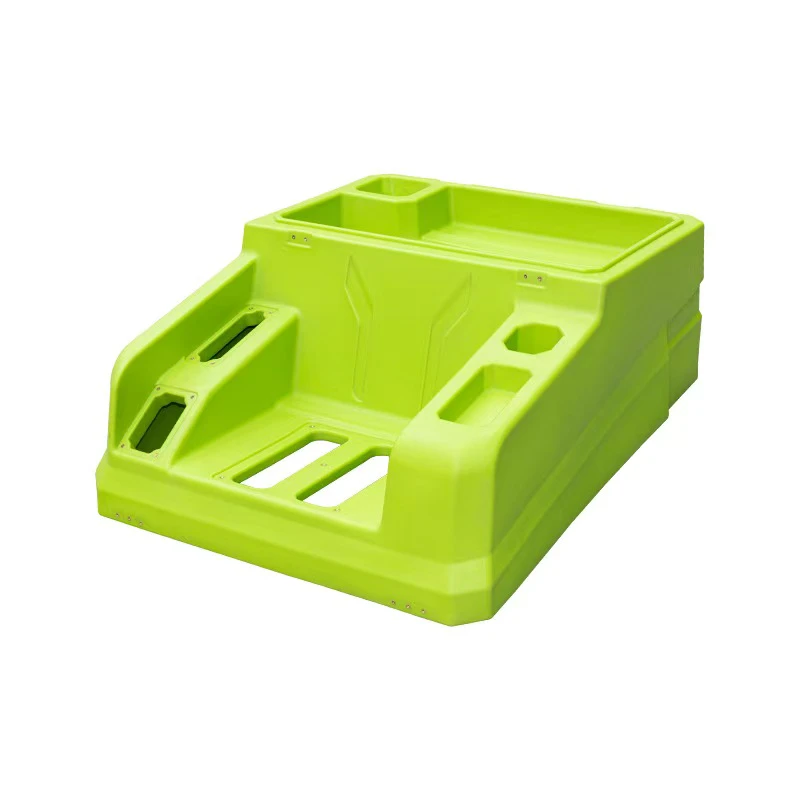
Send the drawing or the existing equipment covers with the annual quantity. The reply is a manufacturability review, a material recommendation and a quotation within 24 hours.
Send the 3D file or drawing with your quantity — manufacturability review and quotation within 24 hours.
Leave a Message