0 Views 2026-09-17 10:40 PPOEM

Atv And Utv Case: 4 mm HIPS Cart Panels from Drawing to Production

This ATV and UTV project started with one question: could cart panels be vacuum formed instead of produced as a fibreglass lay-up? The answer was yes at 4 mm HIPS, and the part went from drawing to approved sample in 8 weeks. Here is the route and the result.
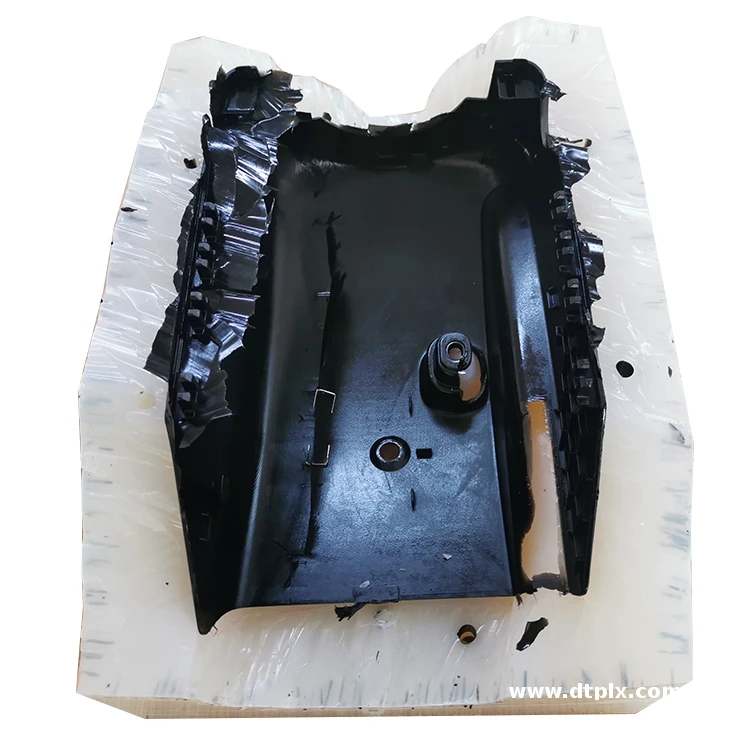
cart panels vacuum forming case for ATV and UTV

The starting point

  • Part: cart panels for ATV and UTV
  • Existing route: a fibreglass lay-up
  • Annual volume: 3600 pieces
  • Problems: high unit cost, long lead time, and variation between batches

What was wrong with the old route

The previous fibreglass lay-up needed several operations to reach finished shape, and every operation added both cost and a chance for variation. Weight was higher than it needed to be, and design changes meant new fixtures each time. For a programme of 3600 pieces a year that is a poor fit.

What we built

ItemValue
Processthick gauge vacuum forming, 5-axis CNC trimming
MaterialHIPS at 4 mm
Forming area usedup to 3,000 × 2,000 mm
Toolingaluminium production mould with a composite sample tool first
Finishtextured as formed
Batch size450 pieces per release
First article8 weeks from drawing release
Documentationdimensional report, material certificate, first article inspection

cart panels formed from HIPS

Process route

  1. The part cools on a jig so the shape is held while the material stabilises.
  2. Trimming is done on 5-axis routers or with a dedicated trim fixture to meet the drawing.
  3. Sheet is dried when the material needs it, then heated to forming temperature on the machine.
  4. The sheet is formed over the mould with vacuum and, where the draw is deep, with plug assist.
  5. Tooling is cut: aluminium for production volumes, composite or printed moulds for samples and first articles.
  6. Drawings are reviewed and a manufacturability report is issued with wall thickness, draft and radii marked up.

Results

  • shortened launch by five weeks
  • First article approved in 8 weeks
  • Tooling amortised inside the first production batch
  • Repeat releases match the approved sample: tooling and programmes are stored against the part number
  • 3600 pieces shipped to date with no dimensional escapes

Lessons from this project

  • The 4 mm was set from the load case, which avoided over specifying the sheet and paying for weight that was not needed
  • Draft and radii were checked before the tool was cut, so the first sample released without hand work
  • The trim line was placed on a flat face, which kept the router inside ±0.2 mm
  • Tooling and programmes are stored against the part number, so repeat releases need no new proving run

What the client said

“The sample arrived on the date we were given and it fitted the assembly on the first try. The cart panels is lighter than the part it replaced and the finish holds up in the field. We now release the cart panels against stored tooling and the paperwork comes with the shipment.”

Frequently asked questions

Could the same route work on a different part?

If the part is a shell, cover, tray or enclosure between 1.5 mm and 12 mm thick, it is almost always worth quoting. Send the drawing and the answer comes back with a material and a tooling plan.

How is the tooling handled between orders?

Tooling, trim fixtures and programmes are kept against the part number for the life of the programme, so a repeat release needs no new proving run.
finished cart panels ready for shipment

Next step

Send the drawing or the existing cart panels with the annual quantity. The reply is a manufacturability review, a material recommendation and a quotation within 24 hours.

Need a part like this?

Send the 3D file or drawing with your quantity — manufacturability review and quotation within 24 hours.
Get a Quote

Leave a Message