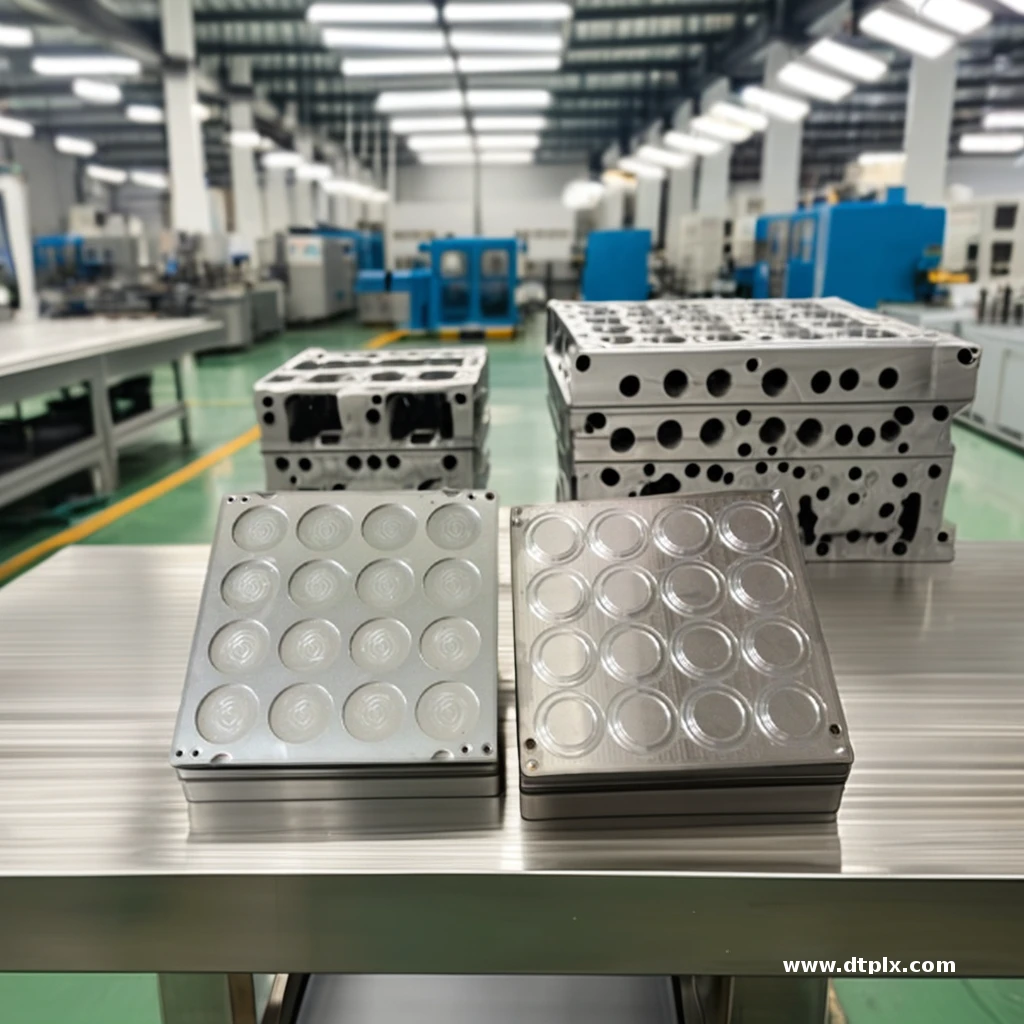
6 mm ABS/PMMA hoppers manufactured for aerospace interiors: ABS/PMMA sheet vacuum formed to drawing, 5-axis trimmed, MOQ 50 pieces, first article in 10-15 working days.
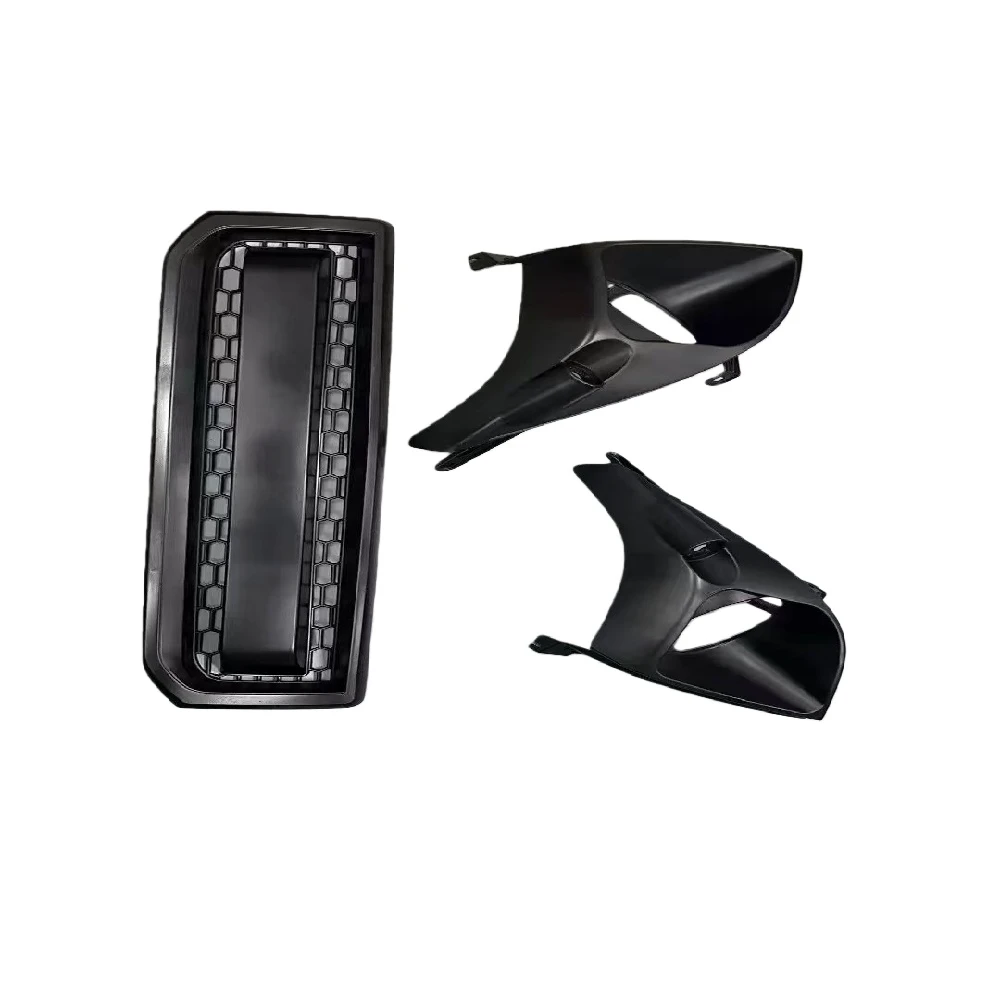
Free QuoteThese ABS/PMMA hoppers are thick gauge vacuum formed parts supplied to drawing for aerospace interiors. They are formed from ABS/PMMA sheet at 6 mm, trimmed on 5-axis routers and inspected against the drawing before packing. Buyers choose this route where a metal fabrication is too heavy, or where injection moulding tooling cannot be justified for the volume.
| Item | Value |
|---|---|
| Product | hoppers |
| Typical application | aerospace interiors |
| Material | ABS/PMMA |
| Standard gauge | 6 mm |
| Gauge range available | 1.5–12 mm |
| Maximum formed size | 3,000 × 2,000 mm |
| Formed tolerance | ±0.5 mm typical |
| Trim tolerance | ±0.2 mm on router cut edges |
| Draft angle | 3 degrees minimum, 5 degrees preferred |
| Finish options | silk screened markings, clear protective film, UV stabilised as formed |
| Minimum order | 50 pieces |
| Lead time to first article | 10–15 working days |
| Tooling | aluminium production tool, composite or printed sample tool |
| Origin | China, export packed |
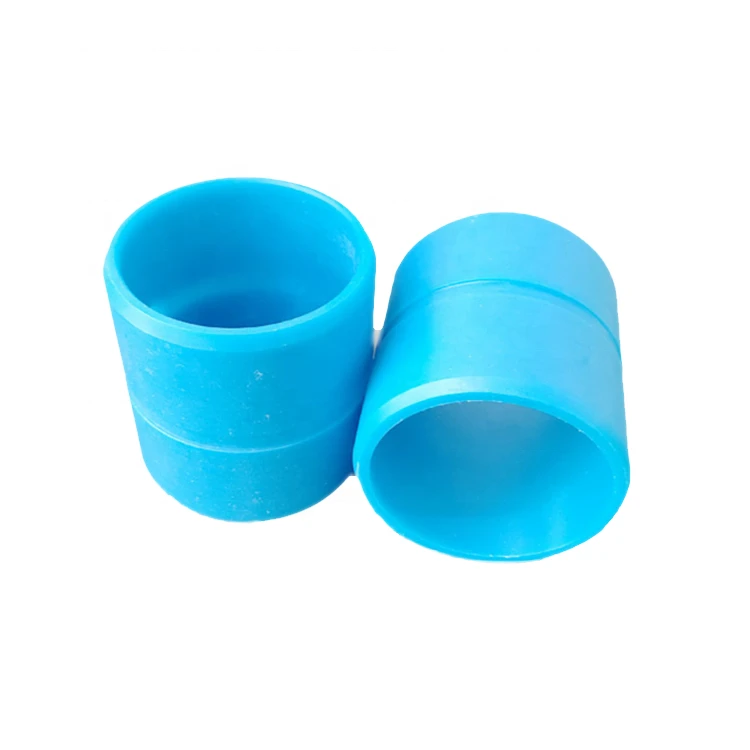
ABS/PMMA combines an ABS core with a hard acrylic cap, so the part has the toughness of ABS and the UV and scratch resistance of acrylic.
Batch releases carry a dimensional report, material certificate and, where agreed, PPAP or ISIR documentation. Moulds, trim fixtures and programmes are stored against the part number, so a repeat order matches the first batch.
Each part is bagged, edges protected with foam, then cartonised for container loading. Standard lead time to first article is 10–15 working days, and repeat releases ship against stored tooling without a new proving run.
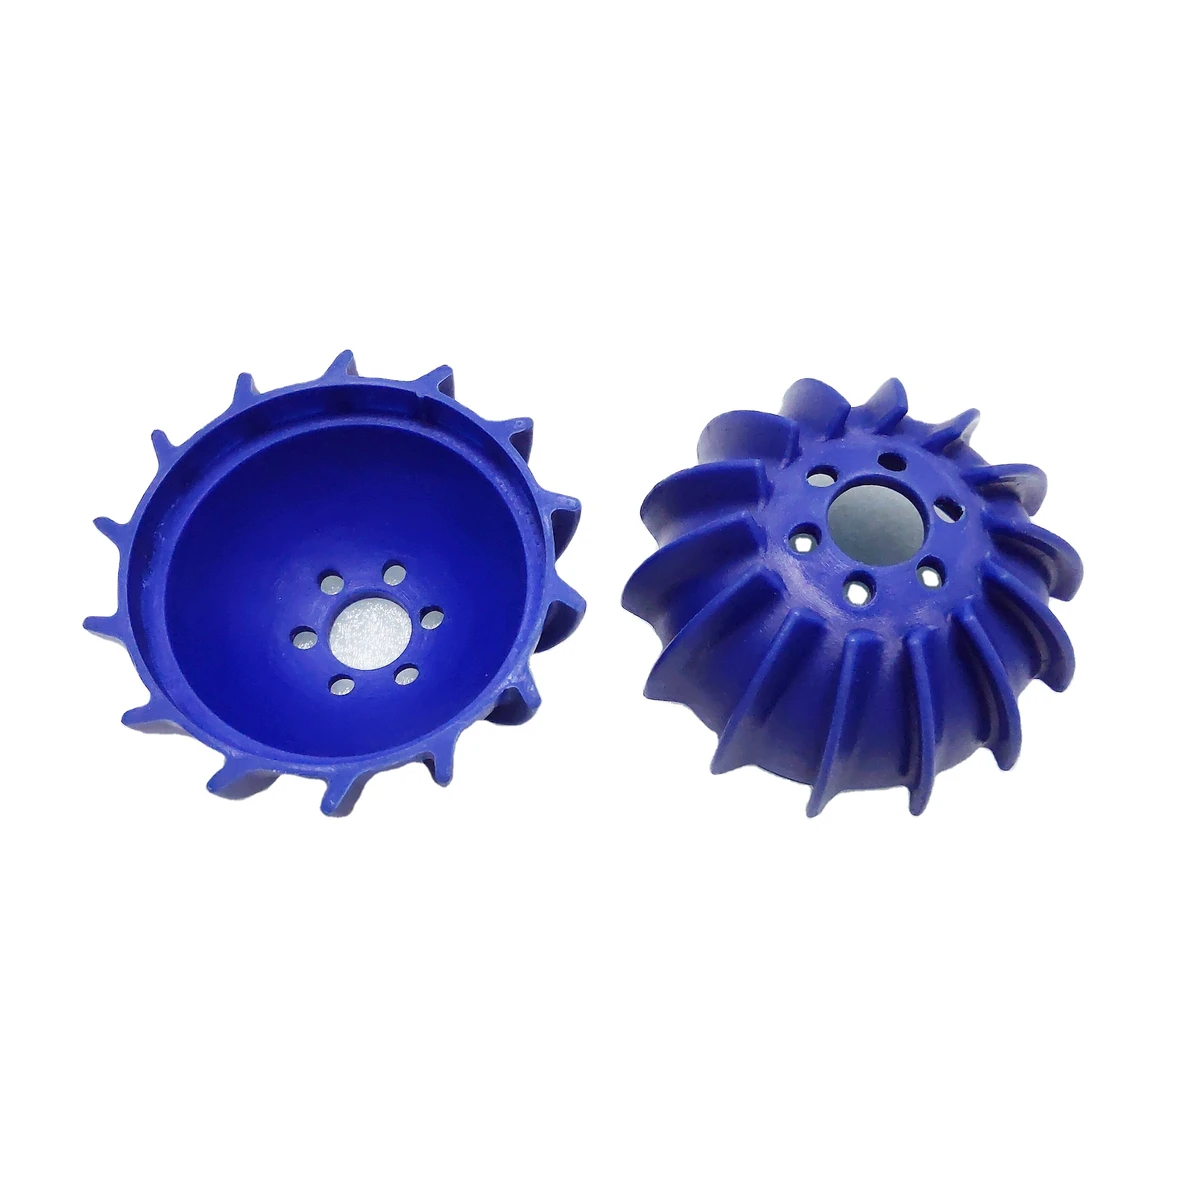
Seven to fifteen working days from drawing release for sample tooling, with production tooling in three to four weeks.
Sample quantities start at one piece off printed tooling. The process pays back from about 25 pieces a year and runs well into several thousand.
Tooling is stored against the part number for the life of the programme, so replacements or spare panels can be released at any time.
Send the drawing or a photo of the current hoppers with the quantity and the finish required. The reply covers material choice, wall thickness, tooling route and price, so the decision is made on a complete picture.
Leave a Message