Home / Product / Thermoforming process / OEM Hoppers LDPE in 3 mm for Laboratory Instruments /
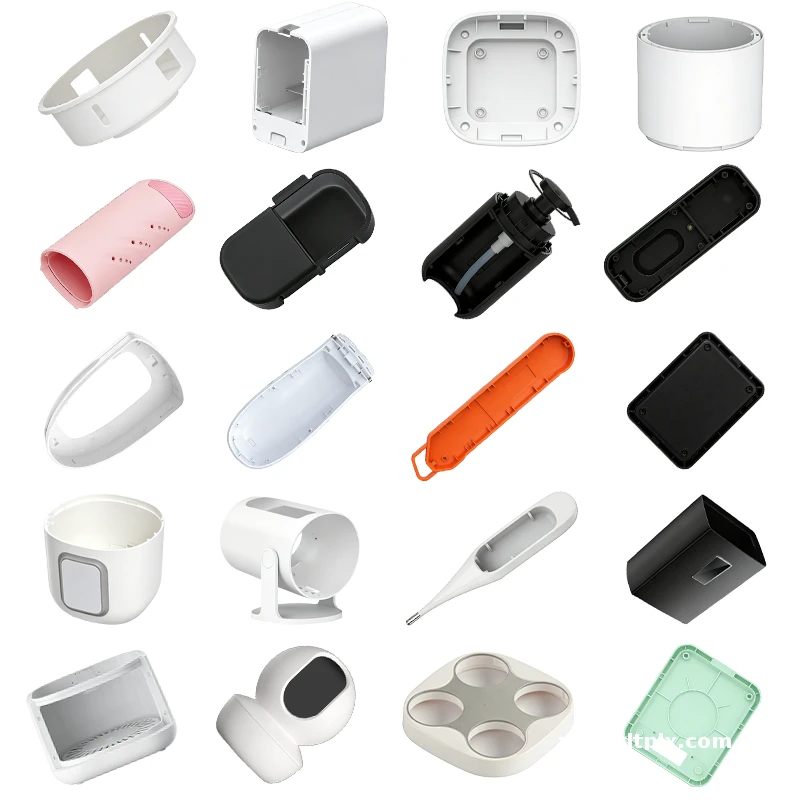
3 mm LDPE hoppers manufactured for laboratory instruments: LDPE sheet vacuum formed to drawing, 5-axis trimmed, MOQ 25 pieces, first article in 10-15 working days.
Free QuoteThese LDPE hoppers are thick gauge vacuum formed parts supplied to drawing for laboratory instruments. They are formed from LDPE sheet at 3 mm, trimmed on 5-axis routers and inspected against the drawing before packing. Buyers choose this route where a metal fabrication is too heavy, or where injection moulding tooling cannot be justified for the volume.
| Item | Value |
|---|---|
| Product | hoppers |
| Typical application | laboratory instruments |
| Material | LDPE |
| Standard gauge | 3 mm |
| Gauge range available | 1.5–12 mm |
| Maximum formed size | 3,000 × 2,000 mm |
| Formed tolerance | ±0.5 mm typical |
| Trim tolerance | ±0.2 mm on router cut edges |
| Draft angle | 3 degrees minimum, 5 degrees preferred |
| Finish options | hot stamped accents, two coat polyurethane paint, satin finish |
| Minimum order | 25 pieces |
| Lead time to first article | 10–15 working days |
| Tooling | aluminium production tool, composite or printed sample tool |
| Origin | China, export packed |
LDPE is flexible and tough in thin section, used for liners and protective covers that have to bend during fitting.
Moulds, trim fixtures and programmes are stored against the part number, so a repeat order matches the first batch. Batch releases carry a dimensional report, material certificate and, where agreed, PPAP or ISIR documentation.
Parts are nested to save freight, with returnable dunnage available on repeat routes. Standard lead time to first article is 10–15 working days, and repeat releases ship against stored tooling without a new proving run.
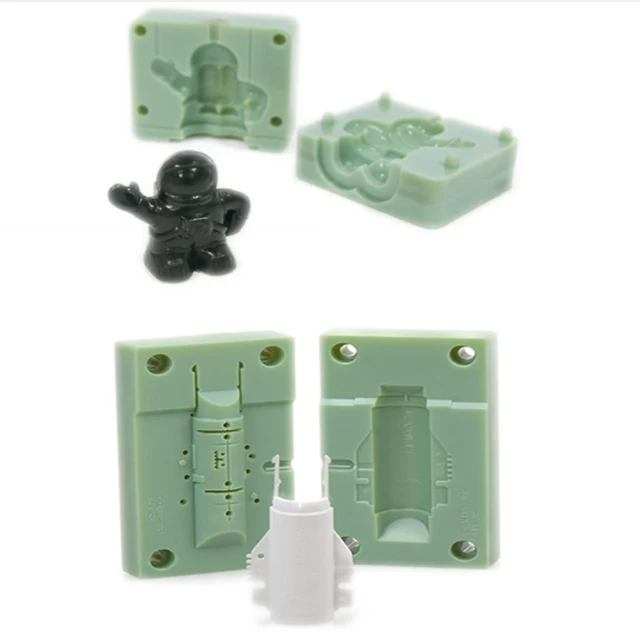
Tooling is stored against the part number for the life of the programme, so replacements or spare panels can be released at any time.
Seven to fifteen working days from drawing release for sample tooling, with production tooling in three to four weeks.
Sample quantities start at one piece off printed tooling. The process pays back from about 25 pieces a year and runs well into several thousand.
Send the drawing or a photo of the current hoppers with the quantity and the finish required. The reply covers material choice, wall thickness, tooling route and price, so the decision is made on a complete picture.
Leave a Message