Home / Wikipedia / 3. Design and Engineering / Draft Angles in Vacuum Forming / Trim cool down time the Right Way – Food Contact Parts /
This guide covers how to trim cool down time on a vacuum formed part: what the designer has to decide, what the mould maker needs to know, and the checks that catch problems before tooling is cut.
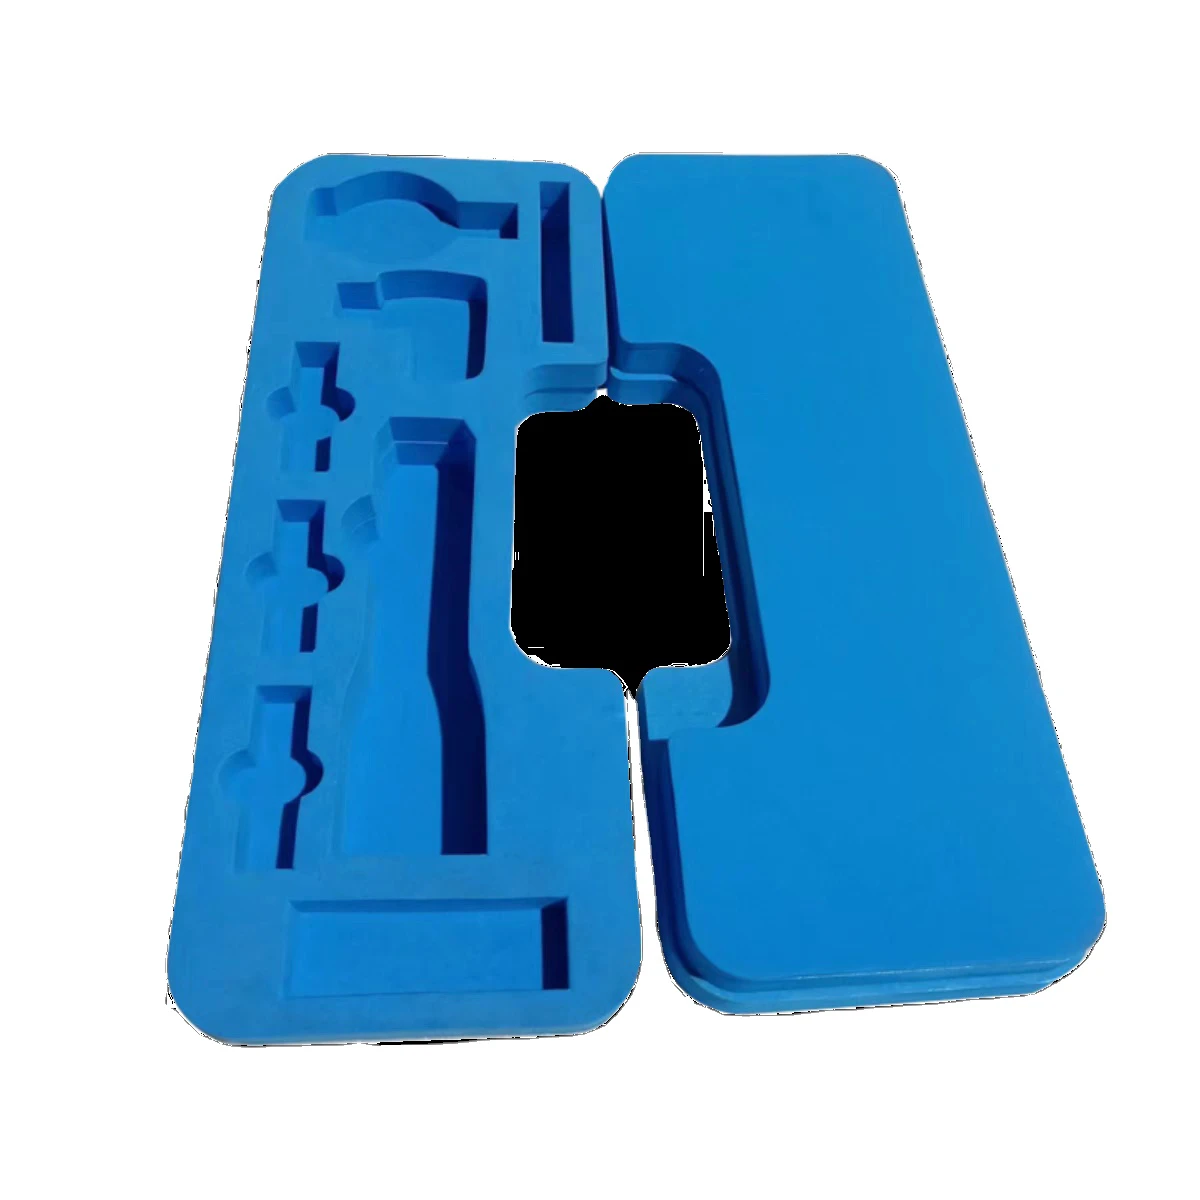
The main effects are on wall thickness, cycle time and how much hand work the part needs after forming. On a thick gauge part these three decide the piece price, so the decision taken here shows up in every release afterwards.
| Item | Value |
|---|---|
| Sheet range | 1.5–12 mm for thick gauge work |
| Forming area | up to 3,000 × 2,000 mm |
| Formed tolerance | ±0.5 mm typical |
| Trimmed tolerance | ±0.2 mm on router cut edges |
| Draft angle | 3 degrees minimum, 5 degrees preferred |
| Corner radius | at least 3 × sheet thickness |
| Cycle time | 60–180 s depending on gauge and material |
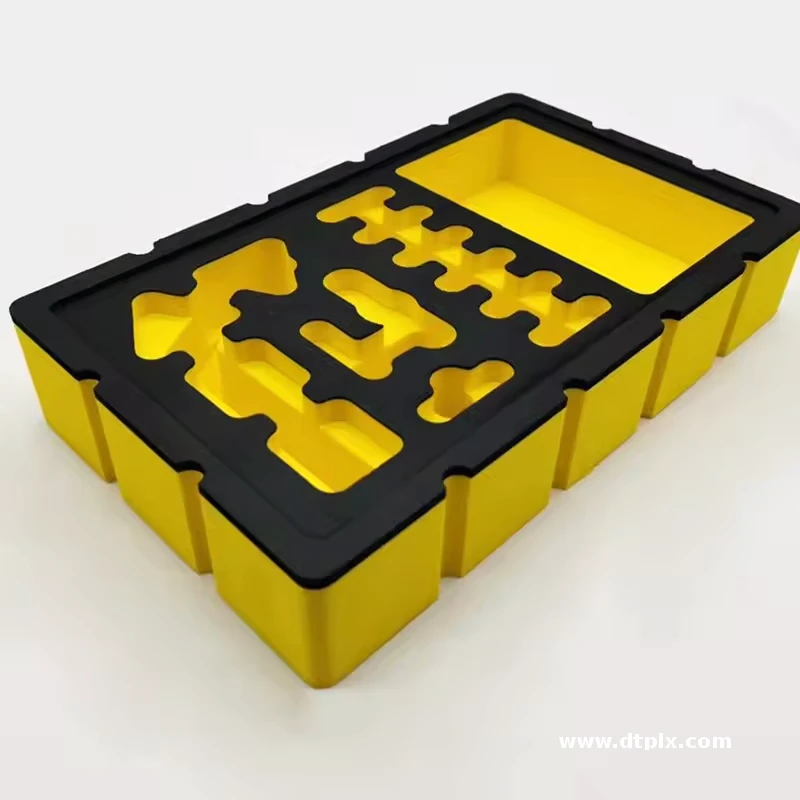
Put the decision on the drawing rather than in an email: state the material and grade, the gauge, the finish, the surfaces that must not carry marks, and the tolerance that applies to the trimmed edges. Where the part has to mate with another component, mark the datum faces so the trim fixture and the inspection report use the same reference. A drawing that states these points removes most of the questions that otherwise surface during sampling.
Yes. Decisions taken at drawing stage move the tooling cost more than any later change, which is why the manufacturability review is done before the tool is cut.
A 3D file, the material if it is fixed, the annual quantity and the finish. With those the answer comes back with a recommended route and a quotation.
Send the 3D file or drawing with your quantity — manufacturability review and quotation within 24 hours.
Leave a Message